Injection Mold Making & Tooling
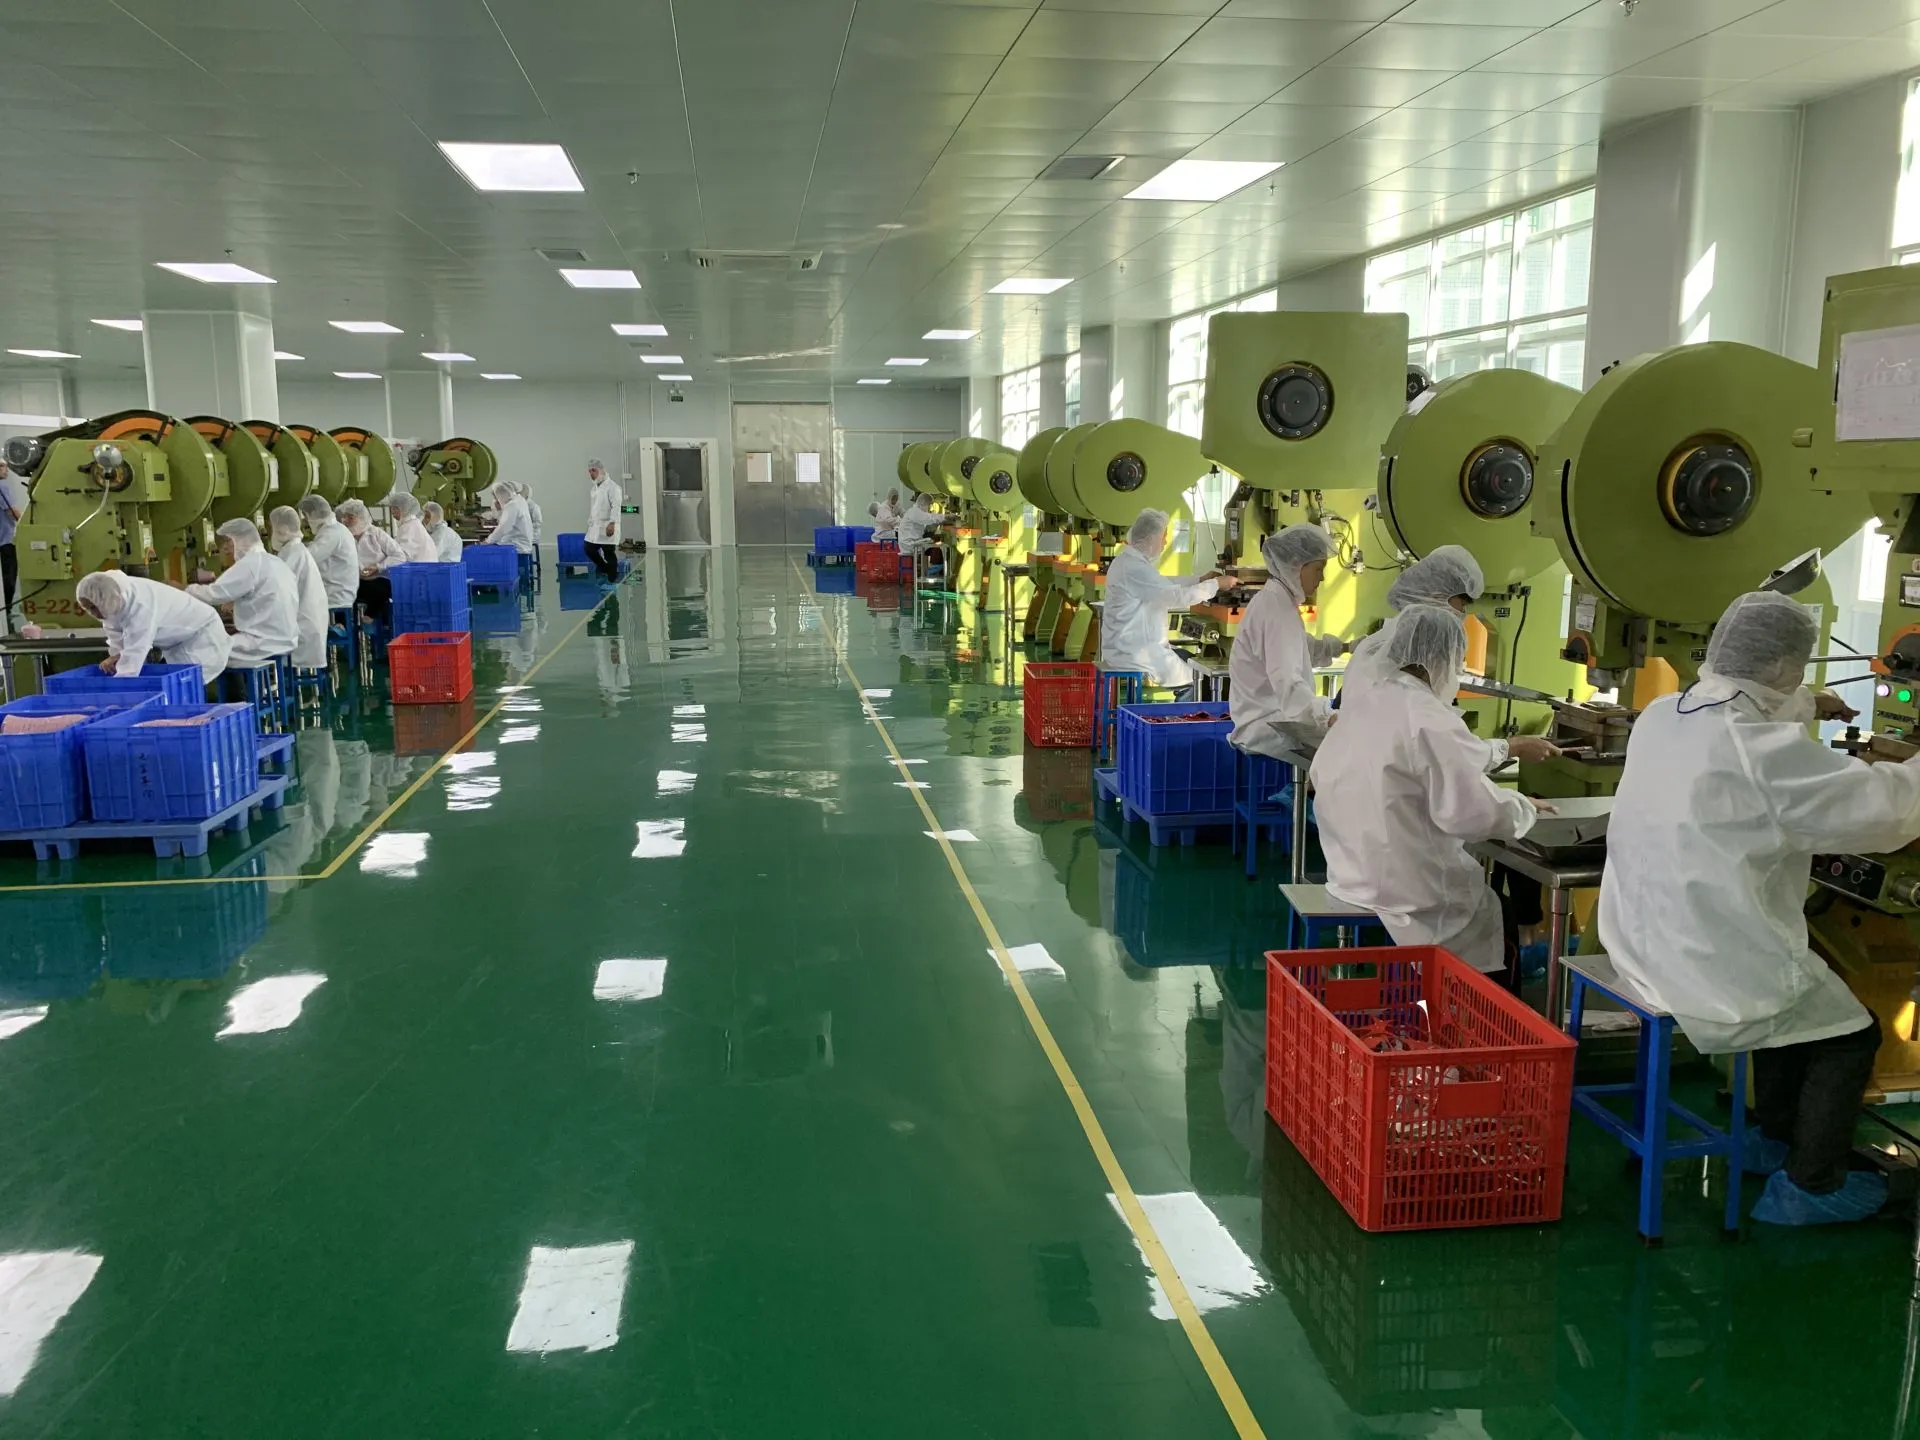
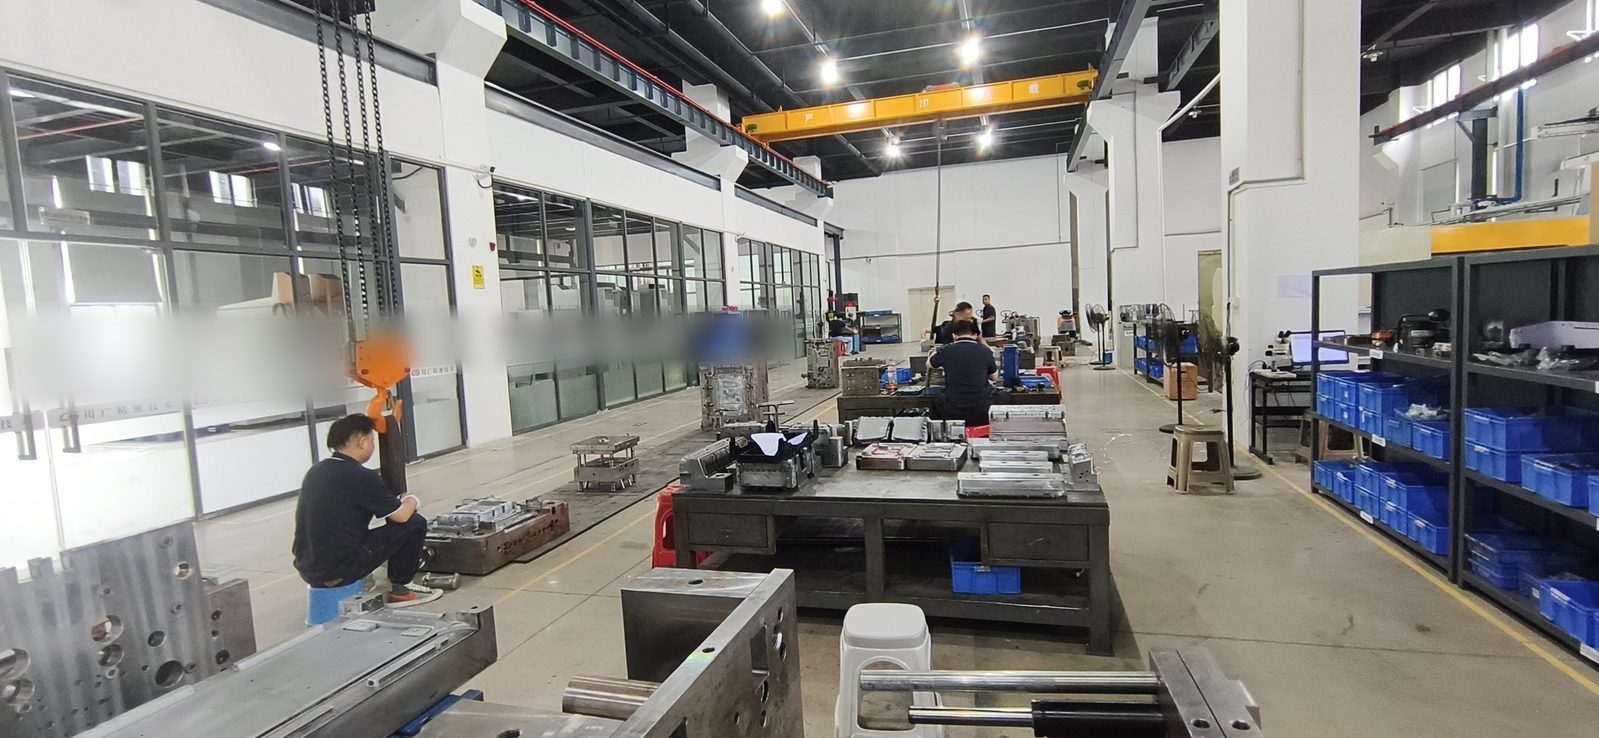
We design and build injection molds in our own shop in Guangdong, China — mold design, 3D machining, EDM, wire cutting, polishing and trial all under one roof. That matters for one reason: when the tool is not right, the people who have to fix it are in the same building as the people who built it.
What we build
| Mold type | Where it is used |
|---|---|
| 2-plate cold runner | The workhorse for straightforward parts and tight budgets |
| 3-plate and pin-point gate | Multi-cavity parts gated away from the visible face |
| Hot runner | Higher volumes, shorter cycles, no runner to trim |
| Insert molds | Metal inserts, threaded bushings, moulded-in fasteners |
| Two-shot / over-molding | Hard-soft combinations, dual-colour buttons, seals |
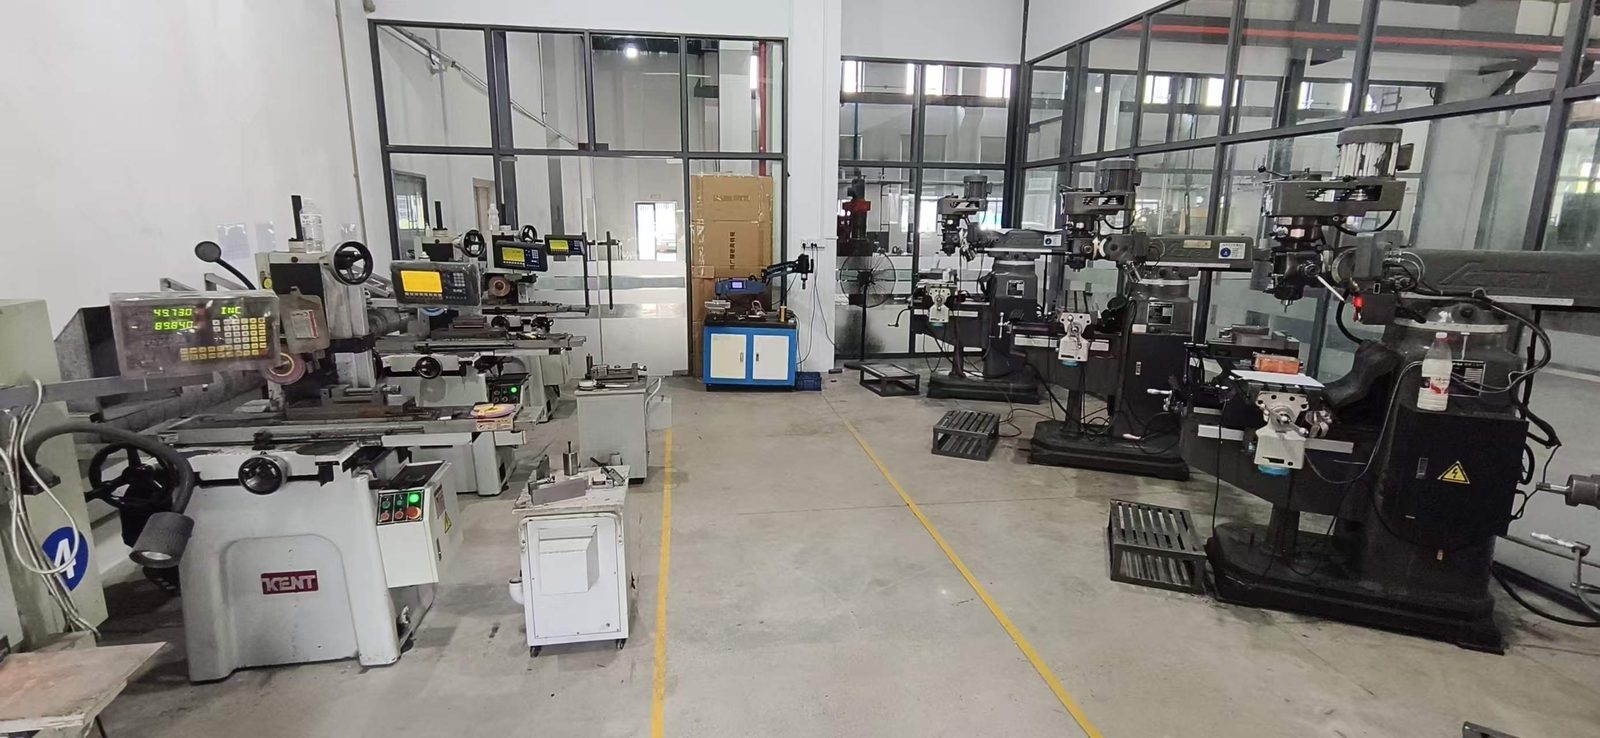
Mold shop equipment
| CNC machining centers | 7 units |
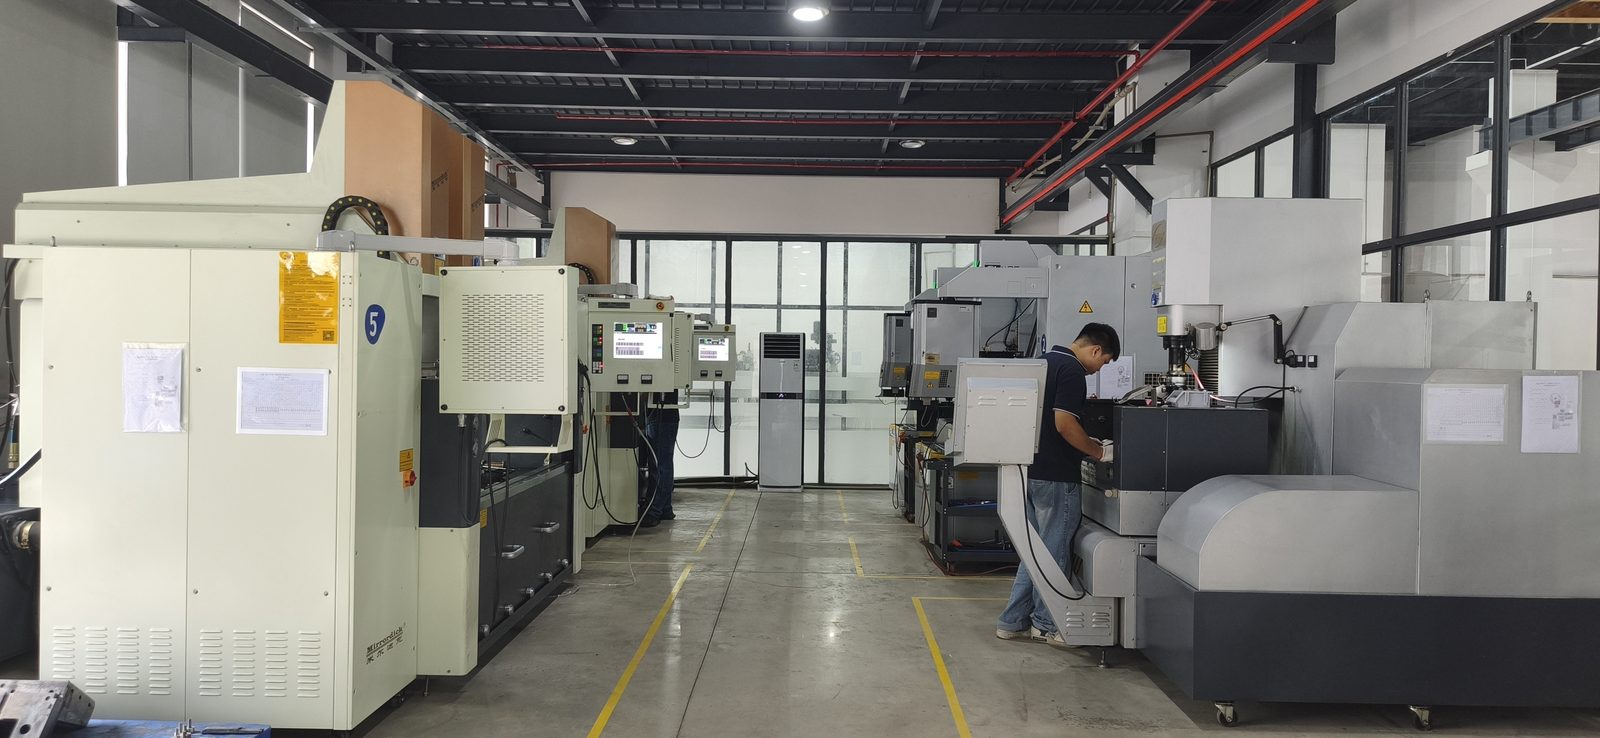
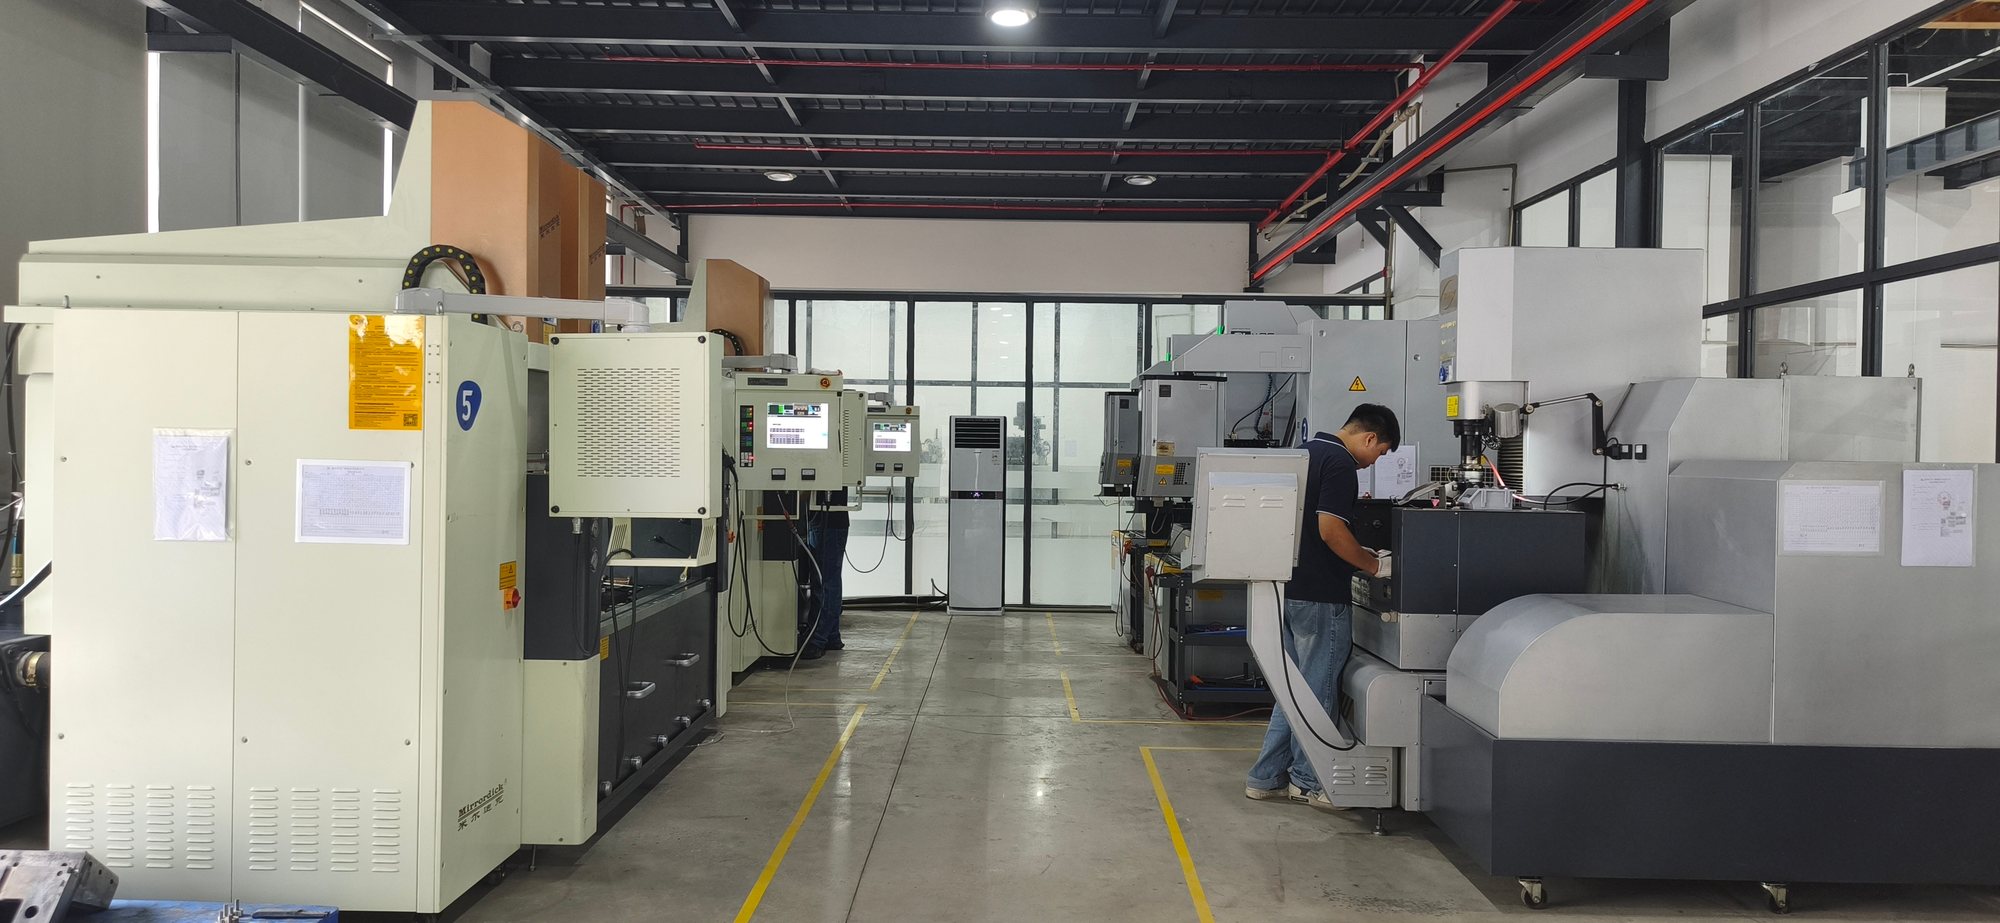
| EDM machines | 7 units |
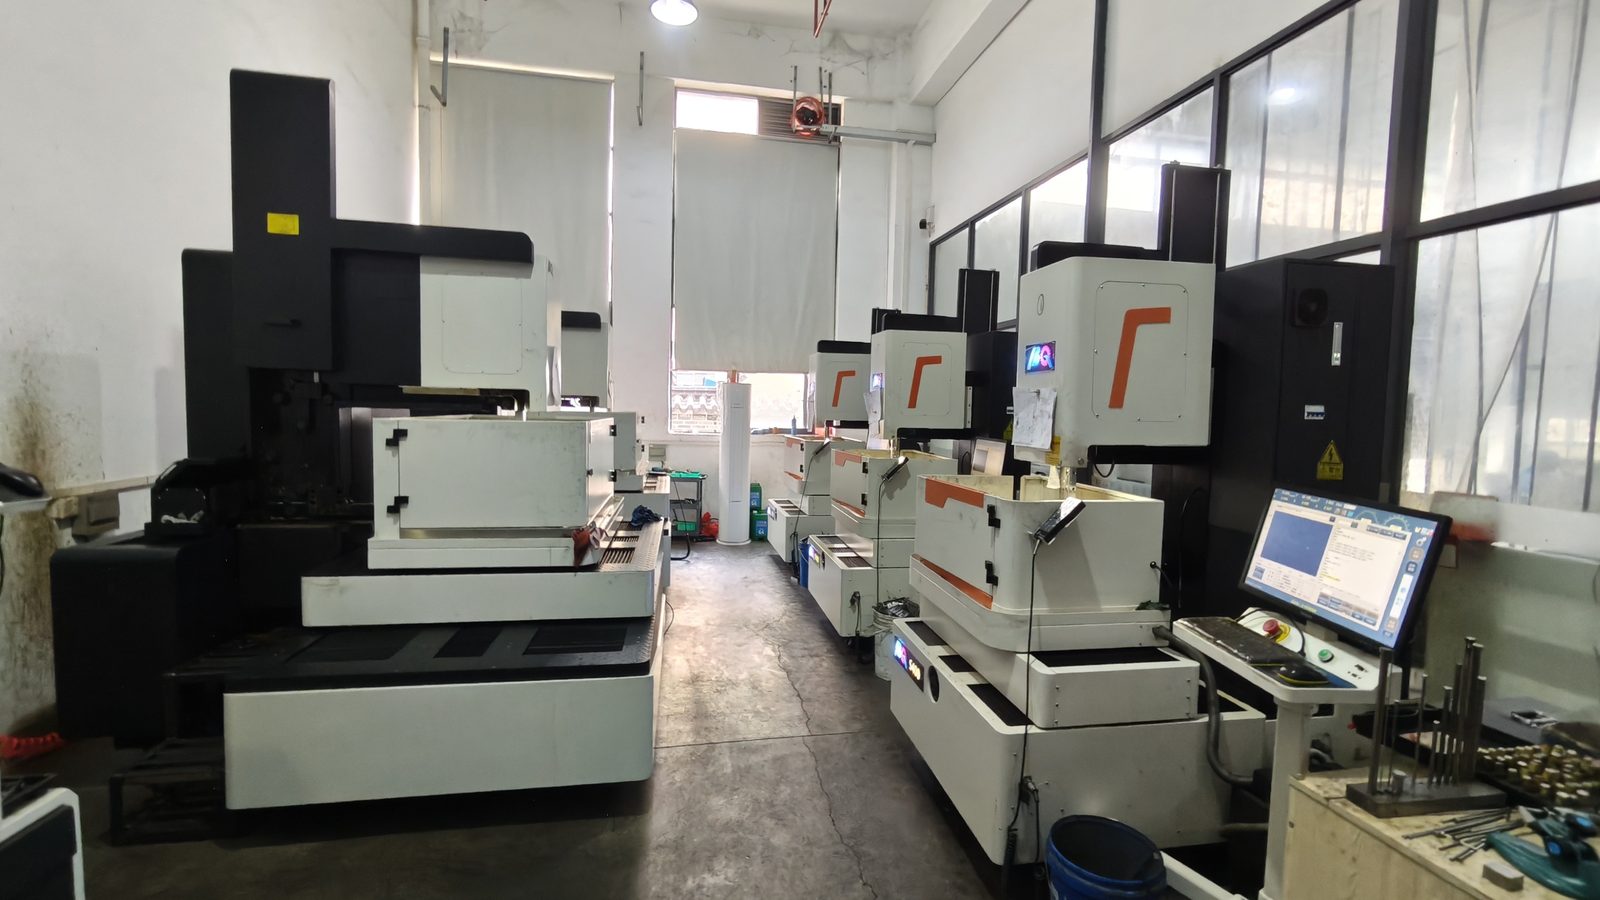
| Wire-cut machines | 11 units |
| Surface grinders | 4 units |
| Milling machines | 4 units |
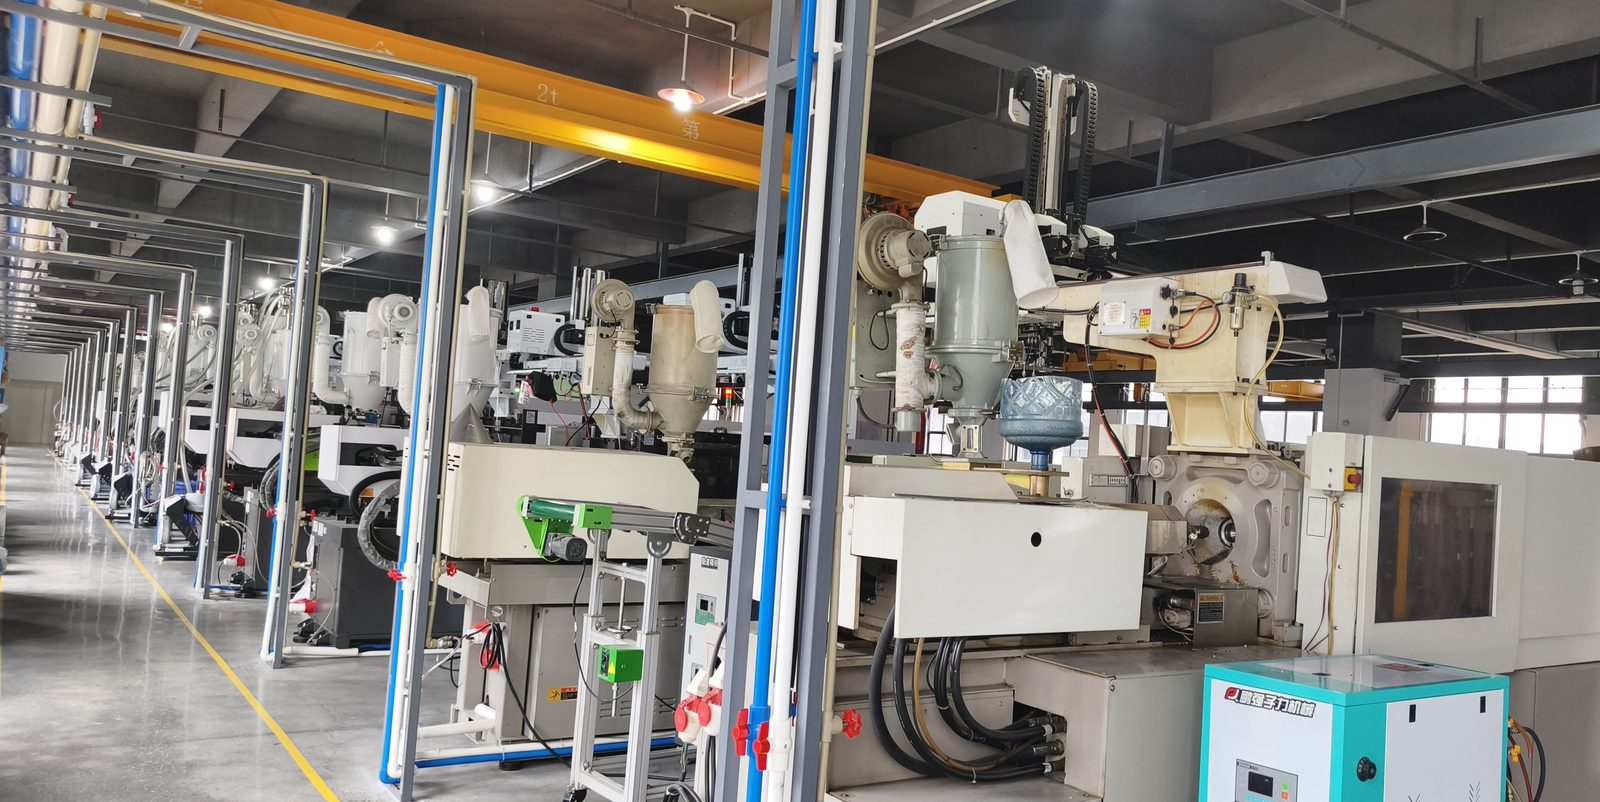
Design and analysis
Mold design is done in UG NX with Moldflow analysis and PowerMILL for the machining paths. Before a block of steel is ordered we have already settled the things that are expensive to change later:
- Wall thickness and where the part will sink
- Gate position and type, and where the weld lines will land
- Cooling layout and predicted cycle time
- Warp and shrinkage allowance, per material
- Draft, ejector positions and where marks are allowed to appear
If your part has a feature that will not mould cleanly, we would rather tell you at this stage. A DFM comment costs you nothing; finding it at T2 costs you weeks.
Steel and standards
Steel grade follows the job. Pre-hardened P20-class steel suits low-volume and pilot tools; hardened 718H, NAK80 and S136-class steels are used where the cavity sees abrasive filled material, high volumes or an optical surface. Hardness, polish grade and expected shot life are agreed before machining starts, not after the first trial.
Trial and validation
- Design review with you, including any changes we recommend to the part itself
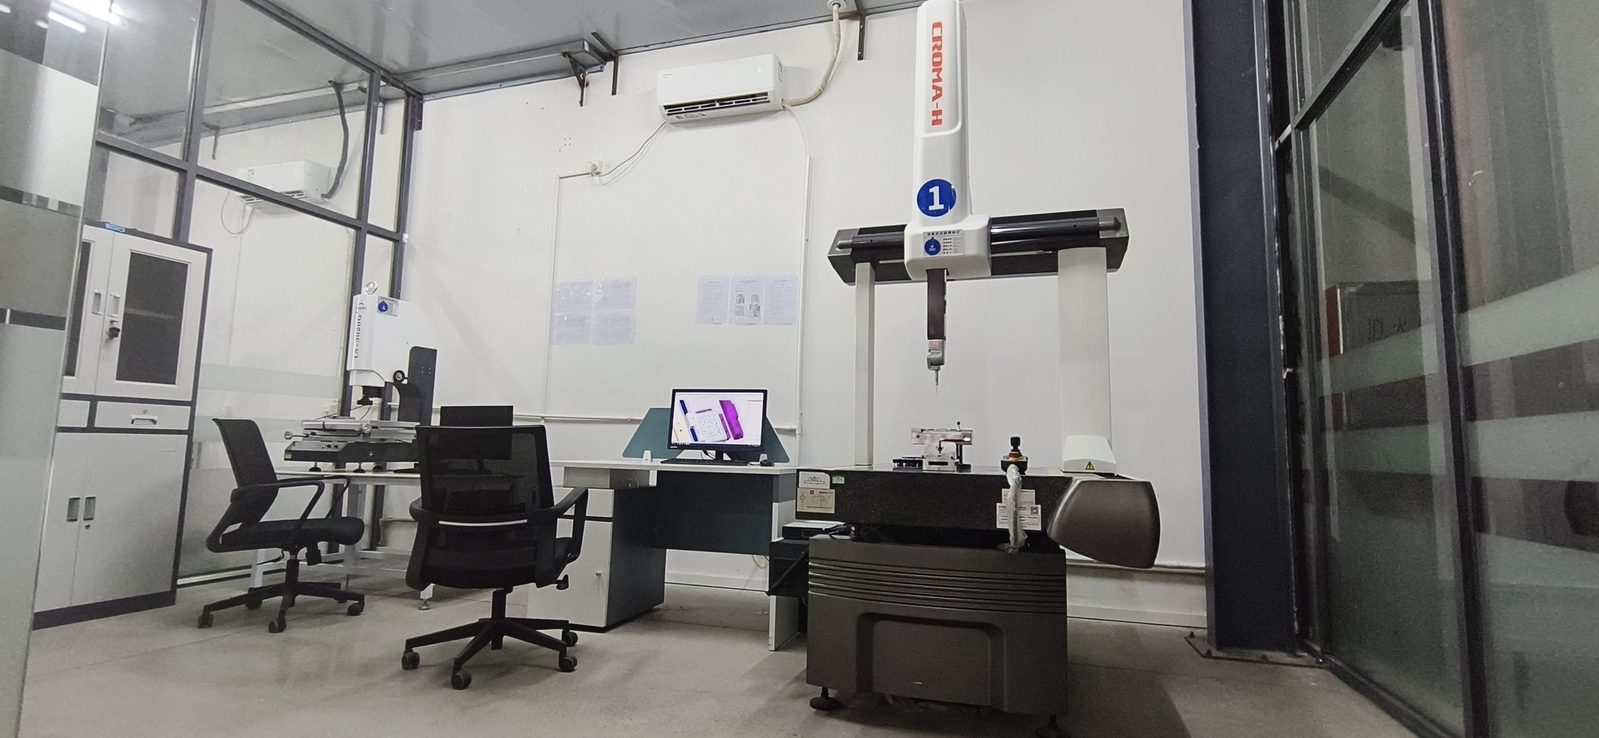
- Machining and fitting in-house, with dimensional checks on the cavity and core
- First trial (T1) — samples, a dimensional report and photos of any visual issue
- Correction and further trials if the part does not yet hold tolerance
- Sample approval — nothing runs in production until you approve a sample
Mold ownership and transfer
When you pay for the tool, the tool is yours. On request we hand over the mold, the 3D data and the mold drawings, so the tool can be run here or moved anywhere else. We would rather keep your business by moulding well than by holding your tool hostage — and we will put that in the quotation.
Frequently asked questions
How long does a mold take to build?
It depends mostly on part complexity, the number of cavities and the surface finish, and we confirm the tooling schedule in the quotation rather than quoting a generic number that later has to be revised.
Can you modify an existing mold?
Yes, if you have the 3D data and the tool drawings, or if the tool can be measured here. Modifications are quoted like a small tooling job.
Do you do Moldflow analysis?
Yes, before steel is cut. It is the cheapest place to find a warp problem, a bad gate position or an impossible cooling layout.
What surface finishes can you put on a cavity?
SPI grades from high polish to heavy matte texture, plus EDM finishes. Tell us the finish you need by name or send a sample part and we will match it.
Can we see the mold before it ships?
Yes. We can send photos and video at each stage, and we welcome visits or third-party inspection during the build.
Related services
- Plastic injection molding services — what the tool goes into
- Custom plastic parts — finished parts and assemblies
Talk to us about your tool
Send a 3D file and we will tell you what the tool needs, what it will cost and where the design might bite you. Request a quote or email amanda@lyetek.com.
Attach a STEP or IGES file and a 2D drawing — or just describe the part and we will tell you what we need. We reply with a DFM review, a tooling price and a piece price.